
In 2025, China’s State Administration for Market Regulation published the results of its 2024 national product quality inspection. For faucets, 59 batches were reported as failing the surface corrosion resistance requirement. This figure highlights the importance of surface quality, but it should not be presented as a failure rate for the entire faucet industry. Nor should nonconforming batches from different test items in the same inspection be simply added together.
For buyers, the more useful questions are:
How will the performance of the products in my order be verified? What does the test result actually prove?
Faucet durability testing should not be reduced to an impressive number of hours or cycles. A useful verification plan needs to connect:
Sample → Test Method → Test Conditions → Acceptance Criteria → Result → Follow-up Action
Only when these elements correspond can a test report provide meaningful purchasing evidence.
Start by Defining the Problem You Need to Control
Surface corrosion, changes in operating feel, leakage after closing, and insufficient flow rate are different problems.
They may occur on the same faucet, but they are not necessarily detected by the same test.
A verification plan should therefore start with the product structure, intended application, and applicable market requirements. The specific performance concern should be defined first, followed by the appropriate test method.
The same national inspection report also covered items such as resistance to operating load, threads, flow rate, and flow-rate uniformity.[1] This shows that finished-product quality has multiple dimensions. A surface corrosion resistance report cannot replace evidence for other performance requirements.
A faucet that operates normally when it leaves the factory should not automatically be assumed to have its long-term performance fully verified.
Development testing, standards-based compliance verification, production monitoring, and pre-shipment inspection can serve different purposes. The people using the results should understand one basic point:
What does each test verify, and what does it not verify?
Salt Spray Hours Cannot Be Directly Converted Into Years of Use
When a supplier provides a faucet salt spray test report, buyers should check the test method, exposure conditions, sample condition, test duration, and evaluation criteria.
A statement such as “passed 500 hours” is difficult to compare with another report if this supporting information is missing. It is also difficult to determine whether the result actually meets a specific purchasing requirement.
ASTM B117 explains that using salt spray results by themselves to predict performance in natural environments often has limited correlation.[2] The published scope of ISO 9227 also states that these tests are not intended to predict long-term corrosion resistance in natural environments or to provide simple rankings of the corrosion resistance of different materials.[3]
Therefore, a test duration should not be multiplied by an arbitrary factor and presented as a number of years that the faucet can be expected to last in a bathroom.
This does not mean salt spray testing has no value.
When its scope and evaluation criteria are clearly defined, it can provide information about the corrosion behavior of surfaces or protective coatings under controlled conditions and can help reveal defects under the specified test environment.
The important point is to interpret the result correctly:
State what the report supports. Do not use one test duration to make conclusions about real-world environments, cleaning practices, or long-term use that the test did not cover.
The Test Sample Must Represent the Actual Product
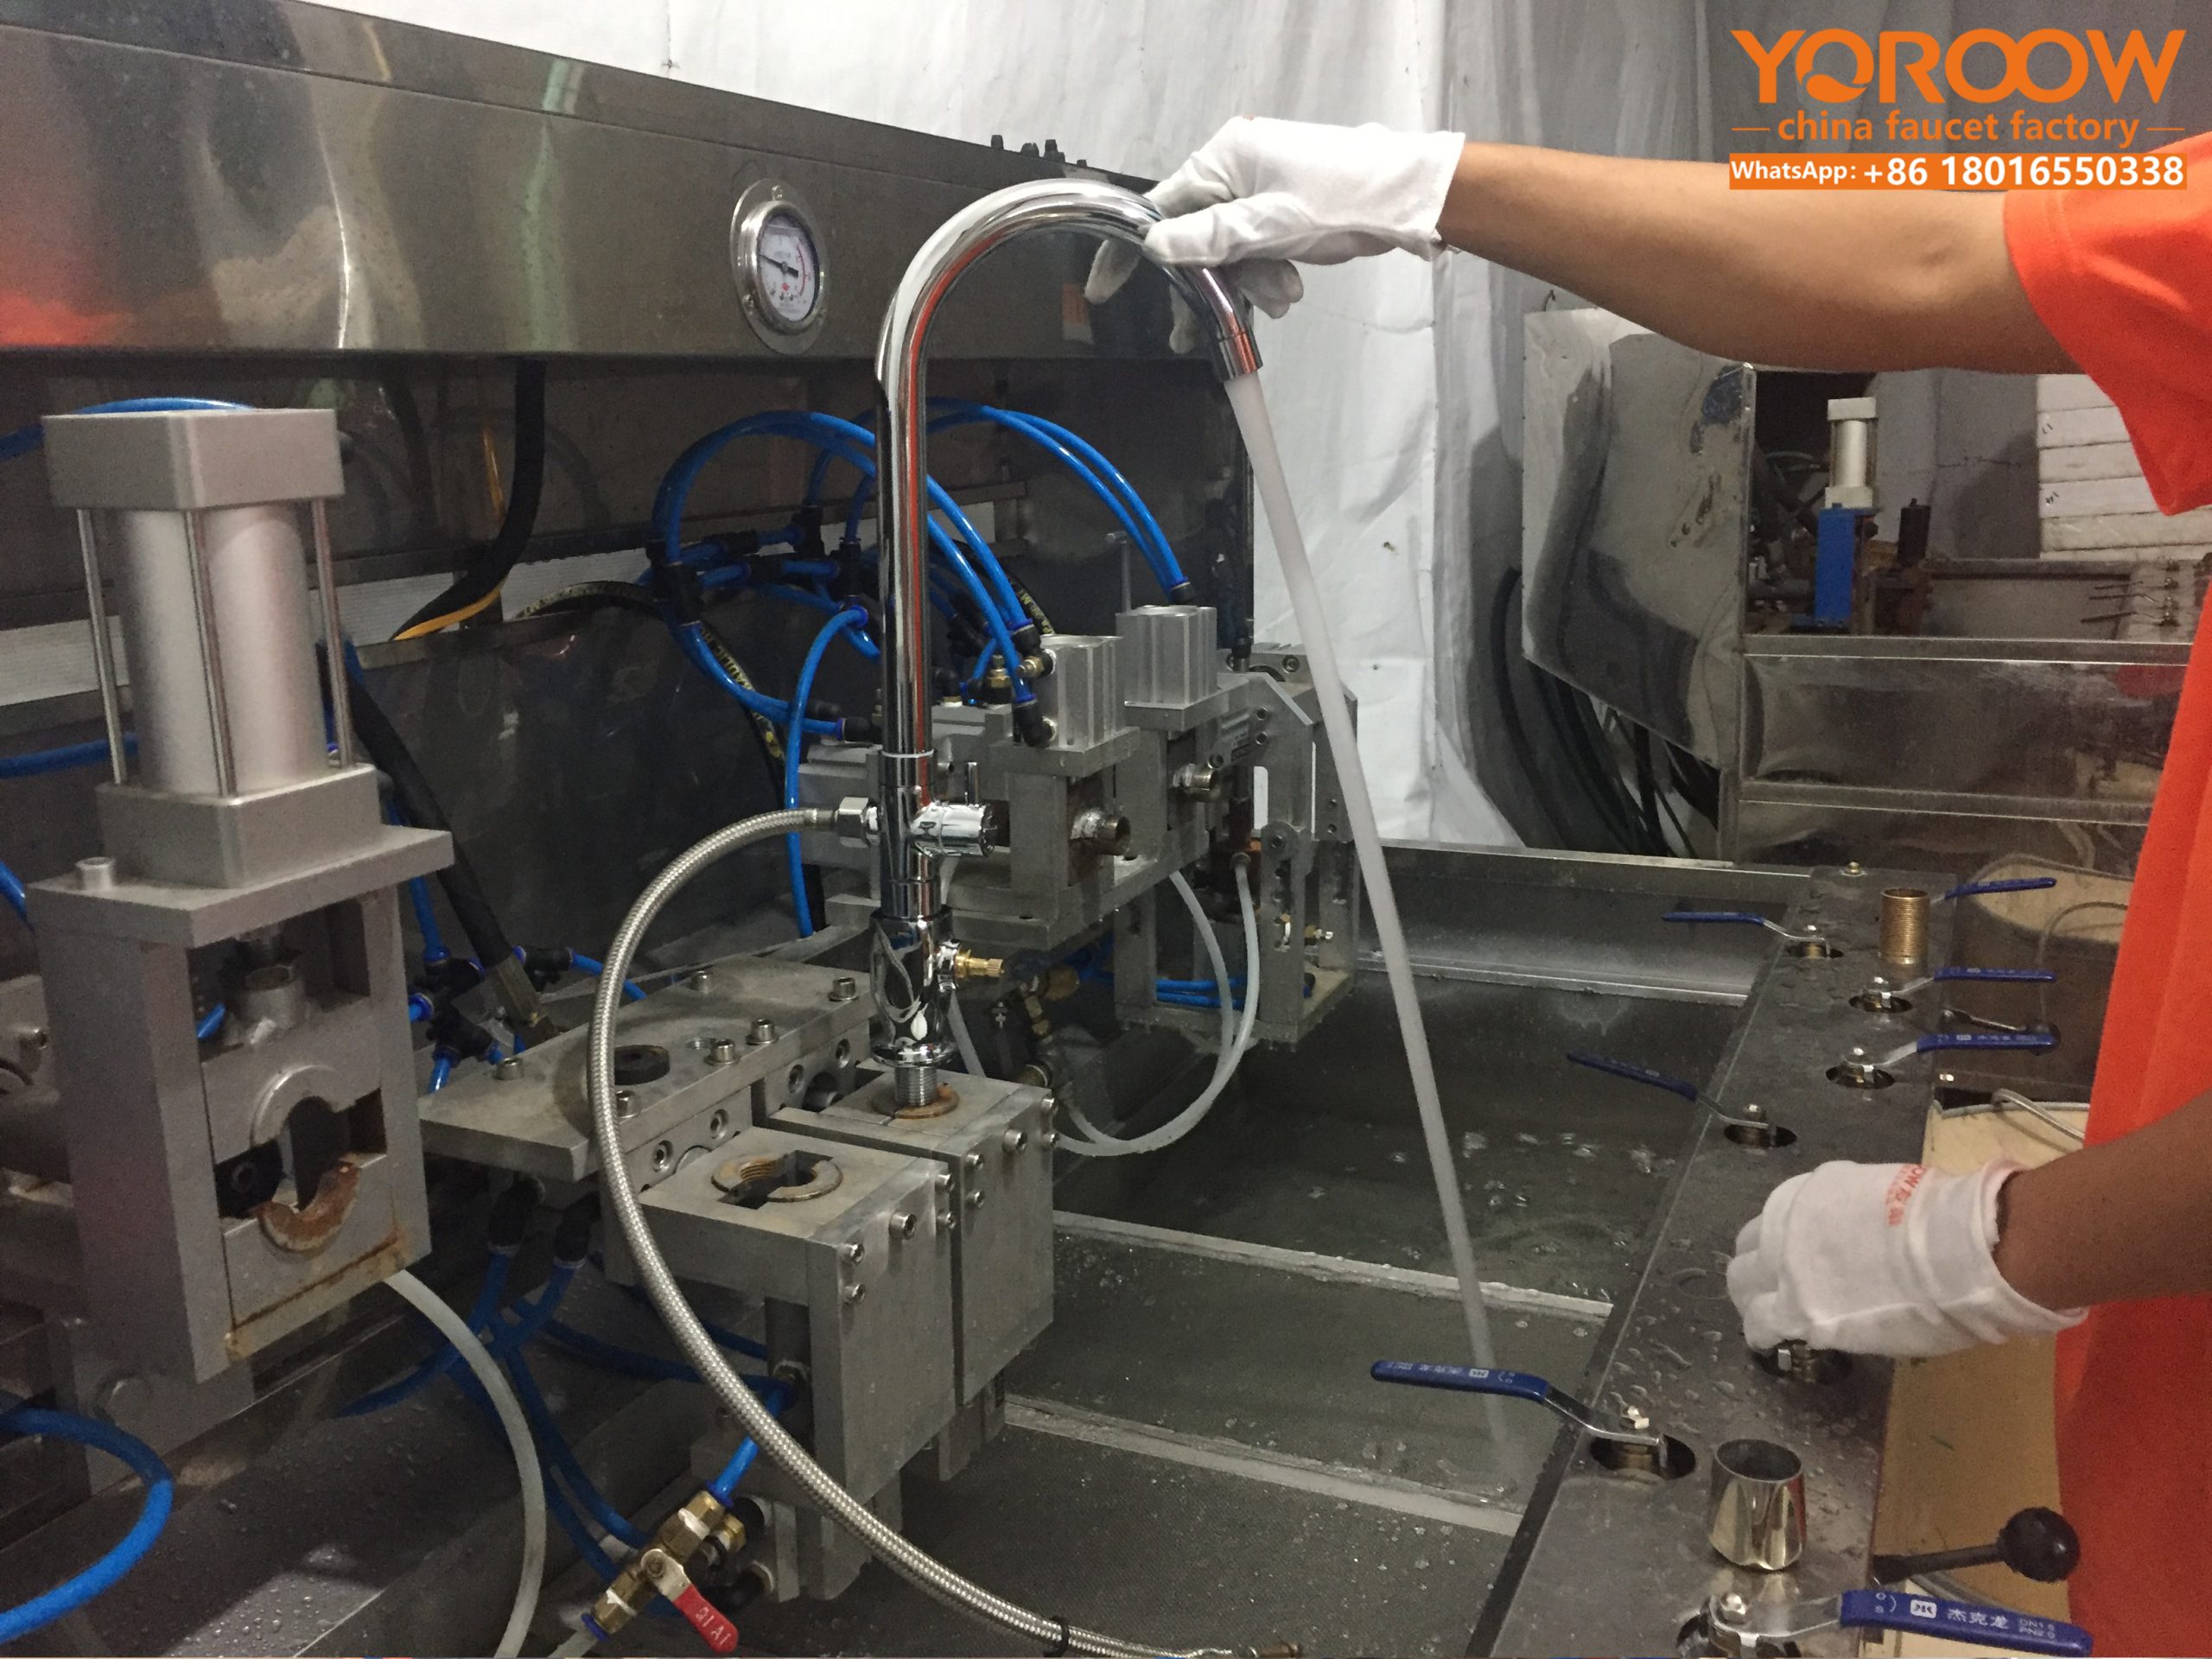
Faucet surface finish testing should clearly identify whether the test object is:
- a test panel or specimen;
- an individual component; or
- a fully assembled faucet.
Each can serve a different purpose, but they cannot automatically represent one another.
If the purchasing concern is the surface condition around joints, edges, or multiple assembled components, the test arrangement should also address those specific areas.
Any special preparation performed before testing should be recorded as well.
For example, if a special development sample uses a different surface treatment route, material, or machining process from the mass-production product, a passing result still needs to be evaluated for representativeness.
The easily overlooked issue is often not the laboratory number itself, but whether there is a clear connection between the tested sample and the actual production product.
A test result can only support a product claim to the extent that the sample behind it is representative.
Before-and-after photographs and specific evaluation locations should also be retained where appropriate. Photos cannot replace the full evaluation, but they can help a purchasing team understand where a change occurred.
When a result cannot be judged from photographs alone, the relevant measurements or observation records should also be retained rather than leaving only a description such as “appearance acceptable.”
Cartridge Cycle Results and Complete Faucet Performance Should Be Reviewed Separately
A faucet cartridge life cycle test primarily evaluates the performance of the control component under specified conditions.
When receiving a cartridge test report, buyers should first confirm the cartridge model, test conditions, and results before considering how the report relates to the faucet being purchased.
Even when the cartridge model is the same, this does not mean that the complete faucet has undergone the same verification under different bodies, handles, connection structures, or assembly conditions.
Complete-faucet evaluation should therefore address operating performance, sealing, and other applicable requirements after assembly.
The test motion, water supply conditions, and acceptance criteria should also have a clear basis.
A cycle count promoted by one brand should not simply be transferred to another faucet as a performance claim. Likewise, laboratory cycles should not be mechanically converted into the actual number of years a faucet will last in every household.
If an abnormality occurs during cycle testing, the record should identify:
when the abnormality occurred, what it looked like, and the condition of the tested sample.
Simply recording the result as “failed” provides limited information for engineering improvement.
Similarly, if a key component is replaced before testing continues, the change should be documented. The later result should not be presented as though the original sample had completed the entire test in its initial configuration.
Flow Rate Data Must Also Be Linked to Conditions and Product Configuration
Faucet flow rate testing may appear to require only one number, but the test object, water supply conditions, and outlet configuration should also be known.
For example, if an aerator, flow restrictor, or another key component changes, it may be necessary to reassess whether the previous flow-rate data still applies.
A product page that lists only one flow rate without identifying the corresponding product version can lead purchasing, testing, and marketing teams to use different sets of data.
A lower flow rate does not automatically mean that a faucet is more suitable for every application.
Handwashing, kitchen use, and other applications have different functional requirements. Water-saving claims and actual user experience should therefore be supported by their respective evidence.
At the sample stage, it may be useful to record both results obtained under a specified standard or agreed test condition and observations from actual-use trials. However, the two types of information should be clearly distinguished.
If production records include water testing, air-tightness testing, or other inspection activities, the test medium, test object, and purpose should also be distinguished. A pressure or air/water description from one document should not automatically be treated as a universal test parameter for every faucet model.
Make the Test Plan Easy to Review
A useful test plan should record more than the number of hours or cycles completed.
Someone reviewing the result later should be able to determine what was tested, which method was used, under what conditions, what counted as passing, and which product version the result belongs to.
| Test Plan Field | What Should Be Defined | What a Missing Field Can Cause |
|---|---|---|
| Sample identity | Model, configuration, batch, quantity | The result cannot be linked to the correct product version |
| Test basis | Method, standard, version, applicable item | Different reports may be compared incorrectly |
| Test conditions & acceptance criteria | Parameters, procedure, pass/fail requirements | Only a test duration or cycle count remains |
| Failure record | Failure stage, symptom, sample condition, and action taken | The reason for failure cannot be reviewed later |
| Production linkage | Mass-production consistency and change-control rules | Initial sample evidence may be reused indefinitely |
This table can serve as a starting point for a test request or internal review. The specific fields should be adjusted according to the project.
For third-party testing, the test scope and final deliverables should also be confirmed before samples are submitted.
Otherwise, discovering after the report is completed that a critical configuration was not tested may require additional samples and testing time.
After a Failed Test, Identify the Cause Before Deciding How to Retest
When a test result does not meet the requirement, the original sample and test records should first be preserved. The test execution and sample identity should then be checked before investigating the product or process cause.
A buyer should not simply keep changing samples until one produces a passing result while ignoring why the earlier sample failed.
When a modified product is retested, the change should be documented:
What was changed, and why is the new test scope sufficient to verify the change?
If the surface pretreatment was changed, its potential impact on the relevant surface-performance requirements should be assessed.
If a control component was replaced, the related functional, sealing, and documentation requirements may also need to be reviewed.
The exact scope of retesting should depend on the actual change and the applicable product requirements. It should not automatically be limited to the single item that failed previously.
Test Reports Should Support Clear Product Claims
The value of a test report ultimately depends on whether it supports an accurate and appropriately limited product conclusion.
For example, a supplier may state that a specific model completed a specified test using the listed method.
However, if the test covered only a particular sample, configuration, and set of conditions, those limitations should not be removed and replaced with a broader claim such as “permanently corrosion-resistant.”
Performance requirements in purchasing agreements should also refer to clearly identified test documents, methods, or acceptance criteria whenever possible. Sales language should not become the only basis for deciding whether a product meets the agreed requirements.
A useful test conclusion is not one that says more. It is one that accurately states how far the evidence can support the claim.
Common Questions
Does a longer test duration automatically mean a better report?
Only when the test methods, samples, conditions, and acceptance criteria are sufficiently comparable can the results be meaningfully compared.
Results from different test methods or different materials should not be simply ranked, and test duration should not be directly converted into product service life.
If there is a cartridge test report, is complete-faucet testing still necessary?
This depends on the applicable requirements and the specific product configuration.
A cartridge test report mainly describes the performance of that component under specified conditions. It does not automatically cover the complete faucet body, assembly method, or other components that determine finished-product performance.
Can national inspection data be used to judge a factory that was not inspected?
No.
Inspection results describe the published samples and test items covered by the inspection. They cannot be used by themselves to determine whether a particular supplier that was not inspected has compliant or noncompliant products.
The specific supplier still needs to provide and verify evidence for the actual product, test scope, and applicable requirements.
Sources
[1] 市场监管总局 2024年27种产品质量国家监督抽查情况通报。
[3] ISO 9227:2022 官方范围说明。